Home › Applications › Ozone Water Treatment › Pharmaceutical Purified Water
Pharmaceutical Water & High-Purity Systems

Ozone Sanitisation for Pharmaceutical Purified Water Systems

Engineered ozone systems for microbial control and sanitisation of Purified Water storage tanks, distribution loops and return lines.

Ozone is integrated as part of the complete PW system — including circulation, dissolved ozone monitoring, sanitisation sequencing, deozonation and controlled release back to production.
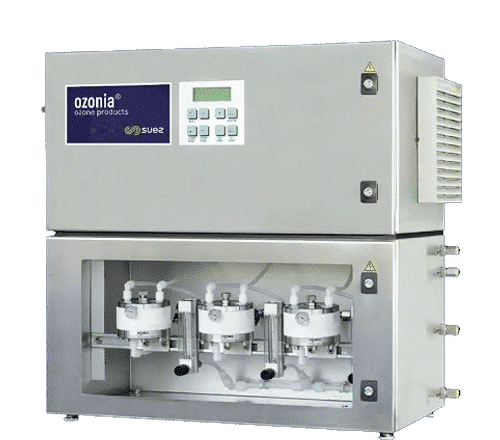
Ozonia Membrel electrolytic ozone system for pharmaceutical purified water loops
Purified Water Loops Storage, distribution and return-loop sanitisation
Electrolytic Ozone Ozone generated directly from high-purity water
Controlled Deozonation UV or validated ozone-removal strategy before use
Measured & Repeatable Monitoring, interlocks, alarms and sanitisation sequence
More Than Water Generation

Microbiological control must continue through storage and distribution

Producing Purified Water at the treatment plant is only one part of pharmaceutical water-system control.

After generation, water may pass through a storage tank, distribution pipework, valves, points of use and a return line before completing the loop. Every wetted surface therefore becomes part of the microbiological-control strategy.

Continuous circulation, hygienic system design, appropriate monitoring and a defined sanitisation procedure are essential to maintaining microbiological quality throughout the complete system.

Ozone can be incorporated into suitable Purified Water systems as a controlled oxidative sanitisation method, particularly where a cold sanitisation strategy is required and ozonated water can be circulated throughout the complete loop.

Ozone does not correct poor hygienic design.

Dead legs, stagnant sections, inadequate circulation and inaccessible parts of the loop should be addressed as part of the system design rather than relying on a sanitisation technology to compensate for them.

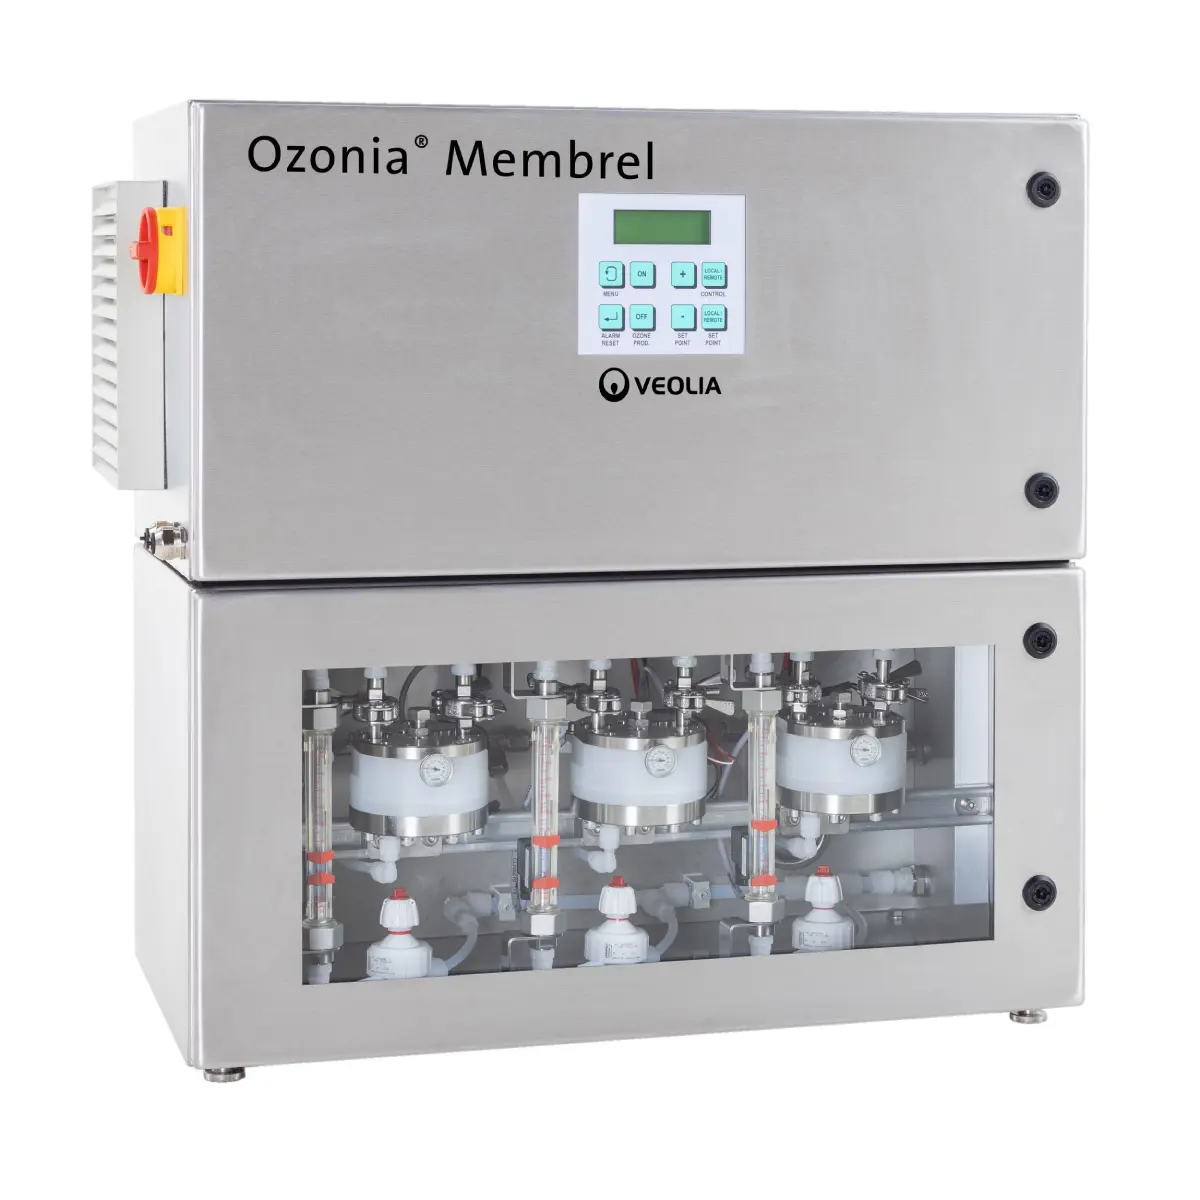
Ozonia Membrel electrolytic ozone generator used for high-purity pharmaceutical water systems
Ozonia Membrel electrolytic ozone technology is designed for pure and ultrapure water loops, including pharmaceutical applications.
PW System Architecture

Where ozone fits within a Purified Water loop

Ozone is normally considered as part of the storage and distribution system rather than as the technology that produces Purified Water itself. The objective is to expose the relevant wetted surfaces to a controlled sanitisation condition and then remove residual ozone before production use.

01
PW Generation
RO, EDI or other qualified purification process
02
Storage Tank
Hygienic storage with continuous circulation
03
Distribution Loop
Continuous circulation through hygienic pipework
04
Points of Use
Production and process take-off points
05
Return Line
Representative return from the complete loop
06
Ozone Control
Sanitisation, monitoring and deozonation strategy
Microbiological Risk

Why PW distribution loops require a sanitisation strategy

Even where the incoming Purified Water meets the required specification, microbiological problems can develop within storage and distribution if system conditions allow organisms to attach and multiply.

01

Storage & residence time

Tank design and water age influence the microbiological environment before water enters the distribution loop.

02

Distribution pipework

Long loops, low-flow sections and unsuitable branches can create conditions where microbial control becomes more difficult.

03

Biofilm development

Once microorganisms establish on wetted surfaces, controlling the attached population may become more difficult than treating free-floating organisms in the water.

04

Points of use

Valves, branches and local operating conditions need to be considered as part of the complete sanitisation and sampling strategy.

05

Reduced production demand

Changes in manufacturing demand can alter flow patterns, residence time and the behaviour of the distribution system.

06

Repeatability

A pharmaceutical sanitisation cycle should be defined, monitored and capable of being reproduced as part of the site's operational and validation strategy.

Application

Where ozone can be used in pharmaceutical water systems

Ozone is particularly suited to applications where the high-purity water can be circulated through a defined system and the dissolved ozone concentration can be monitored at meaningful locations.

01

Periodic loop sanitisation

Ozonated water can be circulated through the storage and distribution loop during a defined sanitisation cycle.

02

Storage-tank control

Ozone can be integrated into tank circulation where the system design and operating philosophy support controlled oxidative treatment.

03

Cold sanitisation

Ozone can provide an alternative sanitisation mechanism where thermal treatment is unsuitable or where the site wants to evaluate a lower-temperature operating strategy.

04

Biofilm management

Oxidative sanitisation can support microbial and biofilm control, but should remain part of a wider hygienic design and monitoring strategy.

Critical Operating Principle

Sanitise with ozone. Remove it before production use.

During a sanitisation cycle, dissolved ozone is deliberately maintained within the loop to expose the required wetted surfaces to the treatment.

Once sanitisation is complete, the system must transition back to production conditions using a defined ozone-removal and verification strategy.

UV deozonation is commonly incorporated into high-purity water systems where rapid destruction of residual dissolved ozone is required before water reaches points of use.

Pharmaceutical water Generator OFF does not automatically mean ozone-free water.

The operating sequence needs to account for dissolved ozone remaining within the tank and distribution system. The return to production should therefore be based on the defined deozonation process and verified residual condition, not simply on elapsed time after the generator stops.

01 Sanitisation Starts Ozone is introduced into the circulating PW loop.
02 Residual Established Dissolved ozone reaches the defined control condition.
03 Contact Maintained The sanitisation condition is maintained for the required period.
04 Deozonation Ozone generation stops and the defined removal process operates.
05 Release for Use Residual condition is verified before normal production resumes.
Ozonia Membrel electrolytic ozone generator for pharmaceutical purified water
Electrolytic Ozone

Ozonia Membrel for high-purity water loops

Ozonia Membrel is an electrolytic ozone technology developed specifically for pure and ultrapure water applications, including pharmaceutical water systems.

Unlike conventional corona-discharge ozone systems, the electrolytic process generates ozone directly from high-purity water rather than requiring an external air or oxygen feed to produce an ozone gas stream.

A side stream from the water loop passes through the electrolytic cell, where ozone is produced and returned into the circulating high-purity water. This architecture is particularly attractive where maintaining the integrity of a high-purity loop is important.

  • Ozone generated directly from water
  • No separate PSA oxygen generator required for ozone production
  • Designed for pure and ultrapure water circulation loops
  • Suitable for controlled periodic or system sanitisation strategies
  • Compact integration into high-purity water systems
  • Can operate with UV-based deozonation architecture
  • Compatible with automated sanitisation sequences
Explore Electrolytic Ozone Systems
Production Mode

Protect the points of use

Where the system architecture uses continuous or background ozonation, UV deozonation can be used to destroy residual ozone before water reaches production points of use.

Sanitisation Mode

Allow ozone through the loop

During the defined sanitisation cycle, the system is configured so dissolved ozone can circulate throughout the required storage and distribution surfaces before the loop is subsequently deozonated.

Monitoring & Automation

The sanitisation sequence matters as much as the ozone generator

A pharmaceutical ozone system is not simply an ozone generator connected to a PW return line.

The complete operating sequence needs to define when ozone can operate, how the sanitisation condition is confirmed, what happens when a sensor or flow condition is invalid, how deozonation is controlled and when the system can return to production.

Dissolved ozone Direct measurement of the ozone residual at the selected control or verification location.
Flow permissive Ozone generation should be interlocked with verified circulation through the intended treatment path.
Pressure & level Appropriate permissives protect the ozone equipment and ensure the hydraulic system is operating correctly.
UV deozonation UV operating status can form part of the production/sanitisation mode logic.
PLC / HMI Automated sequences, setpoints, alarms, trends and operator status can be integrated into the wider water-system controls.
Alarm handling Invalid measurements, low flow or other abnormal conditions should fail the system into a defined safe operating state.
Ambient ozone safety Where appropriate, ambient ozone monitoring and ventilation interlocks protect personnel around ozone equipment.
GMP & Validation Context The ozone system supports the site's validated water-system strategy — it does not replace it.

Sanitisation setpoints, sampling, acceptance criteria, instrument calibration, operating procedures and release back to production should be defined within the pharmaceutical manufacturer's own qualification, validation and quality framework.

Engineering Considerations

What determines whether an ozone PW system will work properly?

01

Hygienic design

The loop should maintain appropriate circulation and minimise dead legs, stagnant branches and areas that cannot be reliably exposed during sanitisation.

02

Loop hydraulics

Flow, pressure, tank volume, pipe volume and return conditions determine how quickly the system can establish and distribute the required ozone residual.

03

Measurement location

A dissolved ozone reading at the tank alone does not necessarily demonstrate that the complete distribution loop has reached the intended sanitisation condition.

04

Ozone demand

Even high-purity systems can exhibit ozone demand from surfaces, contaminants or operating conditions. The measured response matters more than generator output alone.

05

Materials compatibility

Pipework, seals, valve components, membranes and instrumentation should be reviewed for the intended ozone concentration, temperature and exposure duration.

06

Deozonation capacity

The ozone-removal system must be appropriate for the water flow, residual ozone concentration and time available to return the loop to production.

07

Monitoring & verification

Sanitisation should be based on measurable process conditions rather than assuming that generator runtime alone demonstrates treatment of the full system.

Technology Selection

When ozone deserves consideration — and when it may not

The correct sanitisation strategy depends on the existing PW system, manufacturing requirements and site validation philosophy.

Ozone may be a good fit where:

  • A closed-loop PW system can be fully circulated
  • Cold sanitisation is operationally attractive
  • A controlled dissolved ozone residual can be established
  • The loop can be effectively deozonated before use
  • The site wants an automated, repeatable sanitisation sequence
  • Materials are suitable for the proposed ozone exposure
  • Existing microbiological control needs improvement

Ozone may not solve the problem where:

  • The distribution loop contains major dead legs or stagnant areas
  • Water cannot be circulated through all surfaces requiring sanitisation
  • Materials are incompatible with the intended ozone exposure
  • No reliable residual measurement strategy is available
  • There is insufficient time or capacity for deozonation
  • An existing thermal system already performs reliably with no operational reason to change
  • The underlying issue is poor hygienic or hydraulic design
Project Assessment

What we need to review a pharmaceutical PW application

A preliminary assessment normally starts with the hydraulic system, the existing water-treatment architecture and the site's intended sanitisation philosophy.

Water & Loop Data

  • PW distribution flow rate
  • Storage-tank volume
  • Total loop volume
  • Operating pressure
  • Water temperature
  • Pipe diameter and material
  • Return-loop arrangement
  • Relevant water-quality data

Existing System

  • RO / EDI configuration
  • Tank and distribution layout
  • Existing UV equipment
  • Current sanitisation method
  • Points of use
  • Instrumentation
  • Existing PLC / BMS interface
  • Available drawings or P&ID

Operating Requirement

  • Sanitisation frequency
  • Available sanitisation window
  • Microbiological-control objective
  • Current microbial trend or issue
  • Production operating mode
  • Required automation level
  • Residual-ozone monitoring philosophy
  • Site validation requirements
Technical Resources

Related ozone design guidance

Pharmaceutical Water Application

Planning ozone sanitisation for a PW loop?

Send us the loop flow, tank volume, system layout, existing sanitisation method and operating requirements. We can review the ozone generation, circulation, monitoring and deozonation requirements as a complete system.